Initial Entry
The narrow tip enters a straight, pre-drilled pilot hole.
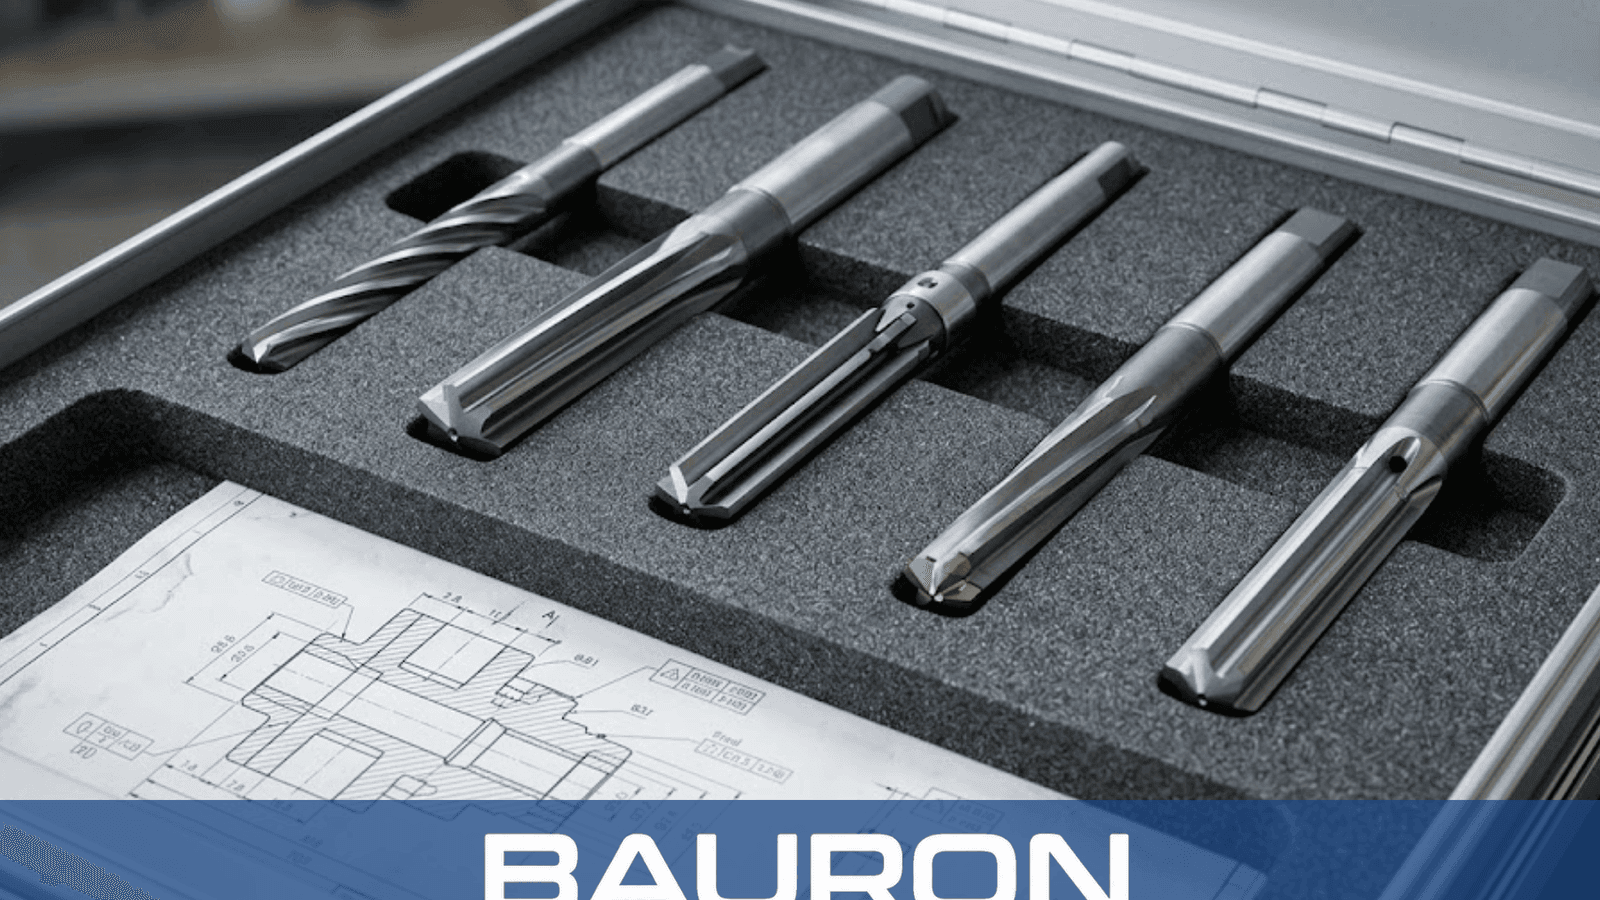
Taper pin reamers are finishing tools used to create conical cavities that match the profile of standard taper pins. The completed hole provides the specified contact for locating and locking mechanical components.
The narrow tip enters a straight, pre-drilled pilot hole.
Conical flutes progressively cut the internal wall to the specified taper as the tool advances.
Straight or spiral flute valleys carry removed material away from the cutting edges.
The finished cavity is sized to seat a matching taper pin through mechanical contact and friction.
Available for 1/4" per foot imperial tapers and 1:50 metric tapers.
Balances toughness and edge retention for manual or machine use.
Provide a positive grip for manual use with T-handle tap wrenches.
Bridge keyways and other interrupted cuts with less tendency to snag than straight flutes.
Finish the tapered surface to support contact with the matching pin.
Limits deflection while reaming deeper conical cavities.
| Specification | Range / Details |
|---|---|
| Diameter Range | Standard sizes #7/0 through #14 |
| Taper Rate | 1/4" per foot imperial or 1:50 metric |
| Flute Geometry | Straight, left-hand spiral, or right-hand spiral |
| Shank Type | Straight with square end, or Morse taper |
| Tolerance | Precision ground to industry taper standards |
| Operation Type | Through-holes and blind taper holes |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS (High-Speed Steel) | General-purpose reaming in mild steel and aluminum. | Economical substrate with impact toughness for hand reaming. |
| Cobalt (HSS-Co) | Harder alloys, stainless steel, and cast iron. | Heat resistance and edge retention suit machine use. |
| TiN Coating | Higher-volume production. | Reduces friction and increases surface hardness to limit tool wear. |
HSS provides toughness for general and manual use, HSS-Co adds heat resistance for harder materials, and TiN can reduce friction and wear in production.
Turn square-shank reamers manually for controlled assembly work.
Provide vertical rigidity and controlled feed for repeatable taper finishing.
Use rigid holders for automated taper-pin hole finishing.
Finishes locating-pin holes used to register machine components.
Prepares tapered holes for pins that lock gears to shafts.
Finishes tapered pin holes used in the assembly of gibs and slides.
Prepares taper-pin holes for components such as gas blocks and sight bases.
Imperial taper pin reamers commonly use a taper of 1/4 inch per foot, while metric versions use 1:50. Match the reamer standard to the specified pin.
Use straight flutes for continuous holes. Spiral flutes can bridge keyways, cross-holes, and other interrupted cuts with less tendency for an edge to snag.
Yes. Start with a straight pilot hole smaller than the minor diameter. Deep tapers may be rough-prepared with stepped drilling to reduce reaming stock.
Unsupported power-drill use is not recommended because the reamer can bind or break and may injure the operator. Use a tap wrench at controlled speed or a rigid stationary machine.
Custom options can include non-standard pin dimensions, taper rates, diameters, and coatings such as TiN or TiAlN.
Bauron provides design and engineering support for taper rates, diameters, flute geometry, shank styles, substrates, and coatings. Share the pin standard and assembly drawing for technical review.
Talk to Engineering