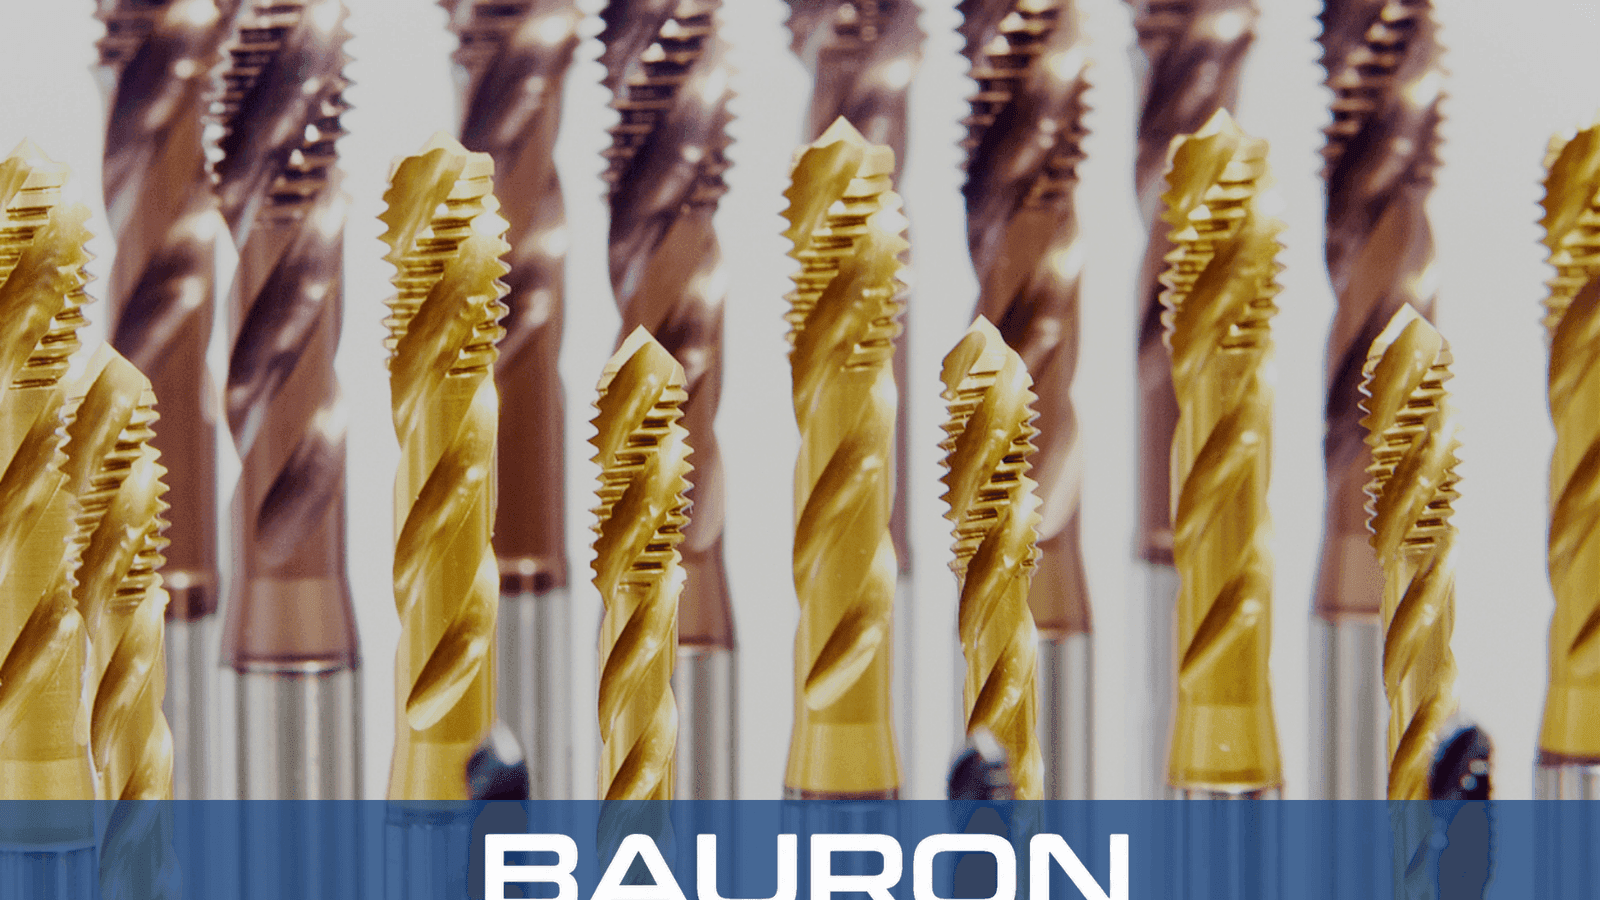
Pressure Engagement
Lobed forming surfaces contact the wall of a precisely sized pre-drilled hole.
A thread forming tap, also called a roll-form or cold-forming tap, creates a thread by plastic deformation instead of chip-producing cutting. Its lobed profile presses a suitably ductile workpiece into the thread form, so pilot-hole size, lubrication, torque control, and material formability are critical.
Lobed forming surfaces contact the wall of a precisely sized pre-drilled hole.
Rotational pressure moves ductile material into the thread crests and roots instead of removing it as chips.
Forming redirects the material's grain flow around the thread profile rather than severing it with a cutting edge.
The process does not generate cutting chips when the material and setup are suitable for thread forming.
Material displacement avoids cut-chip packing and can simplify downstream cleaning.
Retained grain flow and local work hardening can increase thread shear strength in suitable materials and processes.
Fluteless construction provides a larger cross-section than a comparable fluted cutting tap.
Form taps can run at higher speeds than cutting taps in some ductile materials when lubrication and machine control are adequate.
Plastic forming can produce smooth internal thread surfaces without cutting-edge tearout.
| Specification | Range / Details |
|---|---|
| Diameter Range | #0 to 1"+; metric M1 to M30+ available by configuration |
| Body Geometry | Fluteless, multi-lobed form with optional lubrication grooves |
| Thread Forms | UNC, UNF, metric, and custom pitch profiles |
| Shank Type | Straight cylindrical shank with square drive options |
| Pitch Limits | Application-specific GH or metric pitch-diameter limits |
| Pilot Hole Requirement | Form-tap drill size selected for material and target thread percentage |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS-E (Cobalt) | Aluminum, copper, brass, zinc alloys, and selected ductile steels. | Combines toughness and hot hardness for the pressure and friction of forming. |
| Solid Carbide | Stable, high-volume production in compatible abrasive or non-ferrous materials. | High rigidity supports pitch-diameter consistency where the setup can protect a brittle carbide tool. |
| TiCN / CrN Coating | Aluminum, zinc die-cast alloys, and other compatible ductile materials. | Low-friction surfaces help limit galling and workpiece material adhesion on forming lobes. |
Thread forming requires a ductile workpiece. Match tool substrate, coating, lubrication, and pilot-hole size to material elongation, hardness, thread size, and machine rigidity.
Run synchronized tapping cycles in aluminum, copper, and other formable materials.
Use turret-mounted tools to form axial or radial internal threads on turned components.
Produce repeated chipless threads in high-volume component lines.
Forms internal threads in aluminum, copper, brass, zinc alloys, and other suitably ductile materials.
Produces threads in blind cavities without cut chips accumulating at the bottom of the hole.
Creates work-hardened formed threads for automotive, aerospace, and machinery joints where the material supports forming.
Avoids loose cutting chips when threading electronics housings and other assemblies with strict debris controls.
Thread forming requires sufficient ductility. Aluminum, brass, copper, zinc alloys, selected low-carbon steels, some stainless steels, and ductile sheet materials may be suitable after verifying elongation and hardness. Brittle cast iron and hardened alloys are generally poor candidates.
Yes. A forming-tap pilot hole is larger than the cut-tap drill for the same nominal thread because displaced material must flow inward to create the crest. Use the toolmaker's forming-drill chart and adjust for the workpiece material and desired thread percentage.
Material flowing from both flanks can leave a small V-shaped seam or cup at the internal thread crest. It is characteristic of the process, but its dimensions should still meet the part's engineering and inspection requirements.
Forming generates substantial friction and heat. Use a lubricant or coolant with the lubricity and extreme-pressure performance recommended for the workpiece material, coating, and production setup.
Bauron can review custom lubrication grooves, lobe geometries, pitch dimensions, chamfers, substrates, and coatings for a specific forming application.
Bauron provides design and engineering support for forming-lobe geometry, lubrication grooves, pilot-hole strategy, pitch limits, substrates, and coatings. Share material data and process requirements for a technical review.
Talk to Engineering