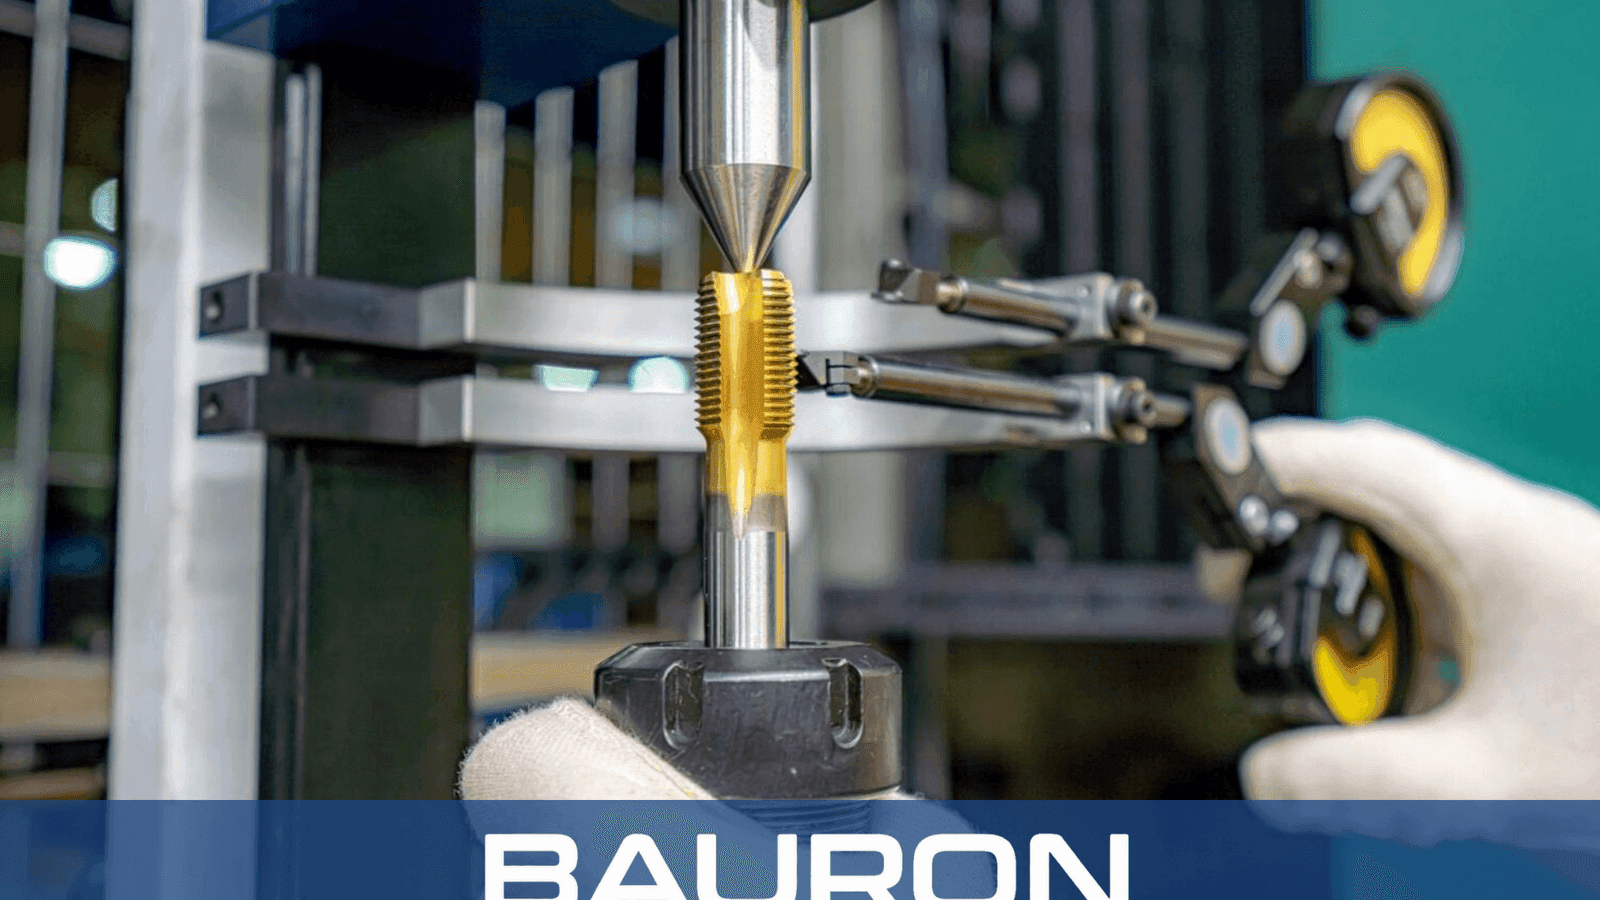
Forward Chip Propulsion
The angular cutting edge directs chips ahead of the tap and toward the through-hole exit.
Spiral point taps are internal thread-cutting tools designed primarily for through-holes. Angular cutting geometry in the lead shears material and pushes chips forward through the hole exit instead of drawing them back along the flute body.
The angular cutting edge directs chips ahead of the tap and toward the through-hole exit.
Shallow flutes behind the point preserve a relatively thick core for torsional rigidity.
The point geometry supports controlled cutting of ductile materials in synchronized machine cycles.
Forward evacuation keeps chips away from the finished threads behind the cutting zone.
The point directs chips out the far side of a through-hole and reduces packing in the flutes.
Shallow flutes retain more core material than deep spiral flutes, improving torsional stiffness.
Core rigidity and forward chip flow support efficient machine tapping under appropriate conditions.
Angular point geometry shears material while directing chips ahead of the tool.
Shallow flutes provide access for application-suitable lubrication or coolant near the cutting zone.
| Specification | Range / Details |
|---|---|
| Diameter Range | #0 to 2"+; metric M1.6 to M50+ available |
| Chamfer Profile | Plug chamfer; 3 to 5 threads standard |
| Thread Forms | UNC, UNF, metric, NPT, and custom pitch profiles |
| Flute Geometry | Angular spiral point with shallow straight flutes |
| Shank Type | Standard square drive or straight cylindrical |
| Tolerance | GH and H-class precision options |
| Material / Coating | Best For | Key Advantage |
|---|---|---|
| HSS-E (Cobalt) | Stainless steel, alloy steel, and titanium. | Hot hardness helps retain the cutting edge in tough, ductile materials. |
| Solid Carbide | High-hardness materials and stable production setups. | Rigidity and wear resistance support continuous machine tapping when alignment is controlled. |
| TiN / TiAlN Coating | Automated through-hole tapping. | Added surface hardness and lower friction can reduce cutting heat and galling. |
Cobalt HSS-E combines toughness and hot hardness, solid carbide adds rigidity and wear resistance in stable setups, and TiN or TiAlN coatings can lower friction in production tapping.
Run synchronized rigid-tapping cycles for through-hole components.
Hold spiral point taps in axial or live-tool turrets for through-hole threading.
Perform repeated threading operations in higher-volume hardware and component production.
Cuts internal threads in open-ended holes while pushing chips through the workpiece.
Handles materials such as aluminum, mild steel, and stainless steel that form continuous chips.
Runs in rigid tapping cycles on milling and turning centers when feed and spindle motion are synchronized.
Fractional or metric sets provide common through-hole tap sizes for production setups.
Spiral point taps push chips forward and are intended primarily for through-holes. Spiral flute taps pull chips toward the entrance and are commonly selected for blind holes.
It is generally unsuitable because forward-directed chips can accumulate at the cavity floor. Use a spiral flute or other blind-hole tap selected for the material and available chip space.
A fractional or metric set gives operators a standardized range of through-hole taps and can reduce tooling changes between jobs.
The name refers to their angular point geometry, which propels chips forward through the workpiece ahead of the cutting tool.
Application-specific options can include non-standard pitches, point geometry, extended shanks, coolant delivery, substrates, and coatings such as TiAlN or TiCN.
Bauron provides design and engineering support for custom thread dimensions, point geometry, shank length, coolant delivery, substrate, and coating selection. Share the through-hole dimensions, workpiece material, and cycle requirements for technical review.
Talk to Engineering